Bidford-on-Avon, Warwickshire. Mon to Fri.01789 224228

Groundwork · specifying the material

Shore hardness: why it is not a preference

Hardness is the one number customers ask for by name, but it is best decided last. It is a balance between holding its shape and releasing the part, so the right answer depends as much on who is demoulding it as on how it looks.

A tradeShape against release
CheckedNot assumed
RecordedAgainst your order
2019Established

Inputs

What actually determines the number?

There are four things to answer, and none is a matter of preference. Once you have answered them, the hardness follows.

01

How the part comes out

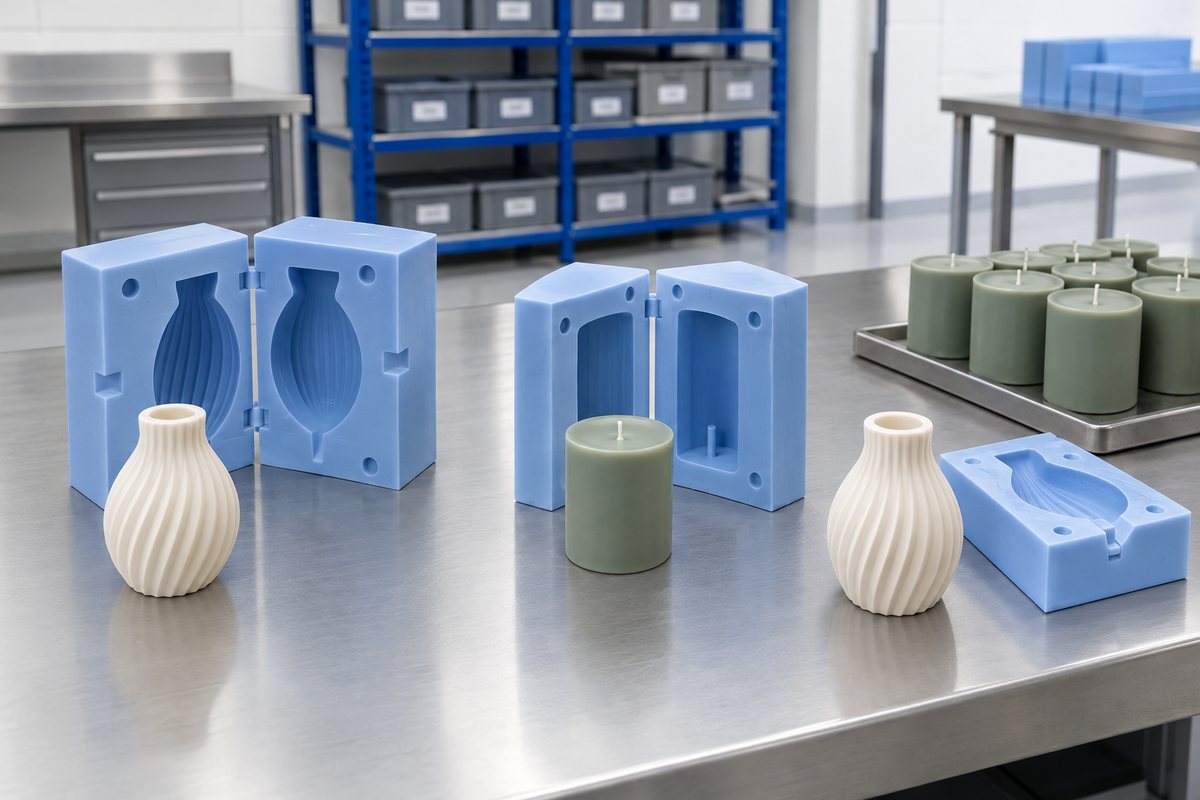
If your part has undercuts, deep relief or re-entrant features, the mould needs to flex to release it, so it must use a softer material. A part that lifts straight out needs no flex, allowing the mould to be harder and last longer.

02

What is being cast in it

A heavy, dense cast can bow a soft mould, leaving the part thicker on one side because the cast material's weight pushes harder. Delicate castings that break on release exert less force and push more softly.

03

How many pulls do you need, and how fast?

A mould that works all shift needs to cope with being handled by someone in a hurry. Softer moulds can tear at thin corners. Harder moulds resist tearing, but they are less forgiving for the person demoulding them.

04

How much detail does it need to hold?

Softer silicone captures fine detail beautifully, but does not retain it as well over time. Harder silicone keeps an arris, or sharp edge, crisp for longer, but is less able to capture fine detail in the first place.

How hardness differs by route

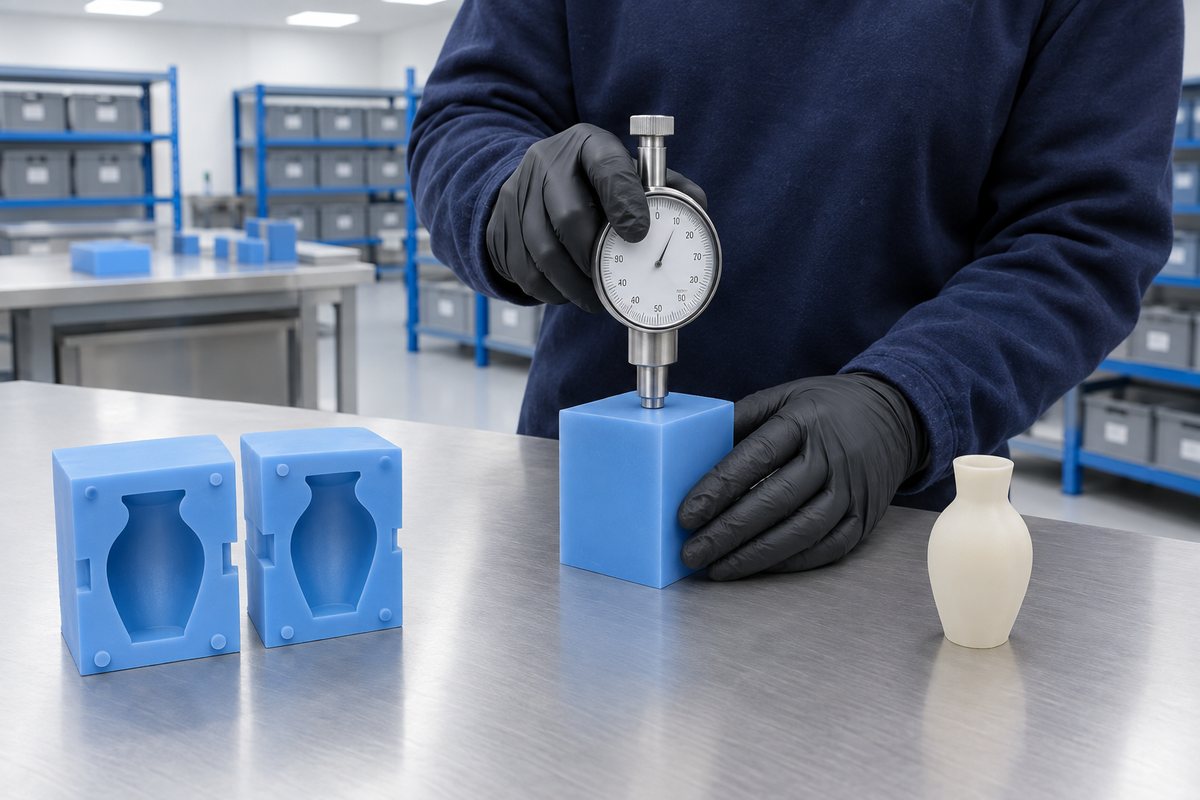
Illustrative example: Soft and firm silicone mould sections showing different release requirements
Mould flexibility depends on shape and cast material

Why no chart

A chart matching grades to applications could be misleading.

It might be tempting to add a table matching hardness values to applications. However, that guidance would be wrong often enough to cause real problems, so we have chosen not to include one.

That is because hardness never acts alone. Wall thickness affects a mould's behaviour just as much as hardness does. In practice, a thick, soft mould can be stiffer than a thin, hard one. Tear strength matters at least as much, and it does not track hardness neatly. So, two moulds with the same hardness but made from different grades can have very different working lives. Cavity geometry changes things again. A soft mould with a deep, narrow feature will grip harder than a firm mould with an open one.

There is also the human factor, which no chart can capture. The same mould can have two very different lifespans: one in the hands of a maker who owns the piece, and another with a production operator at the end of a long shift. Specifying the mould for the first situation but delivering it for the second is one of the most common reasons moulds fail early.

When a previous supplier's hardness value worked for them, it's natural to ask for the same one. We first ask what your mould needs to do rather than simply matching the number. Often, the original number was right. Sometimes it was inherited from a completely different job, and repeating it only repeats the problem. If your mould fails at the same corner every time, hardness is one of the things we will look at, alongside the geometry and how the mould is being used. See design for manufacture for the rest of that conversation.
Checking

Hardness can drift, so we check it.

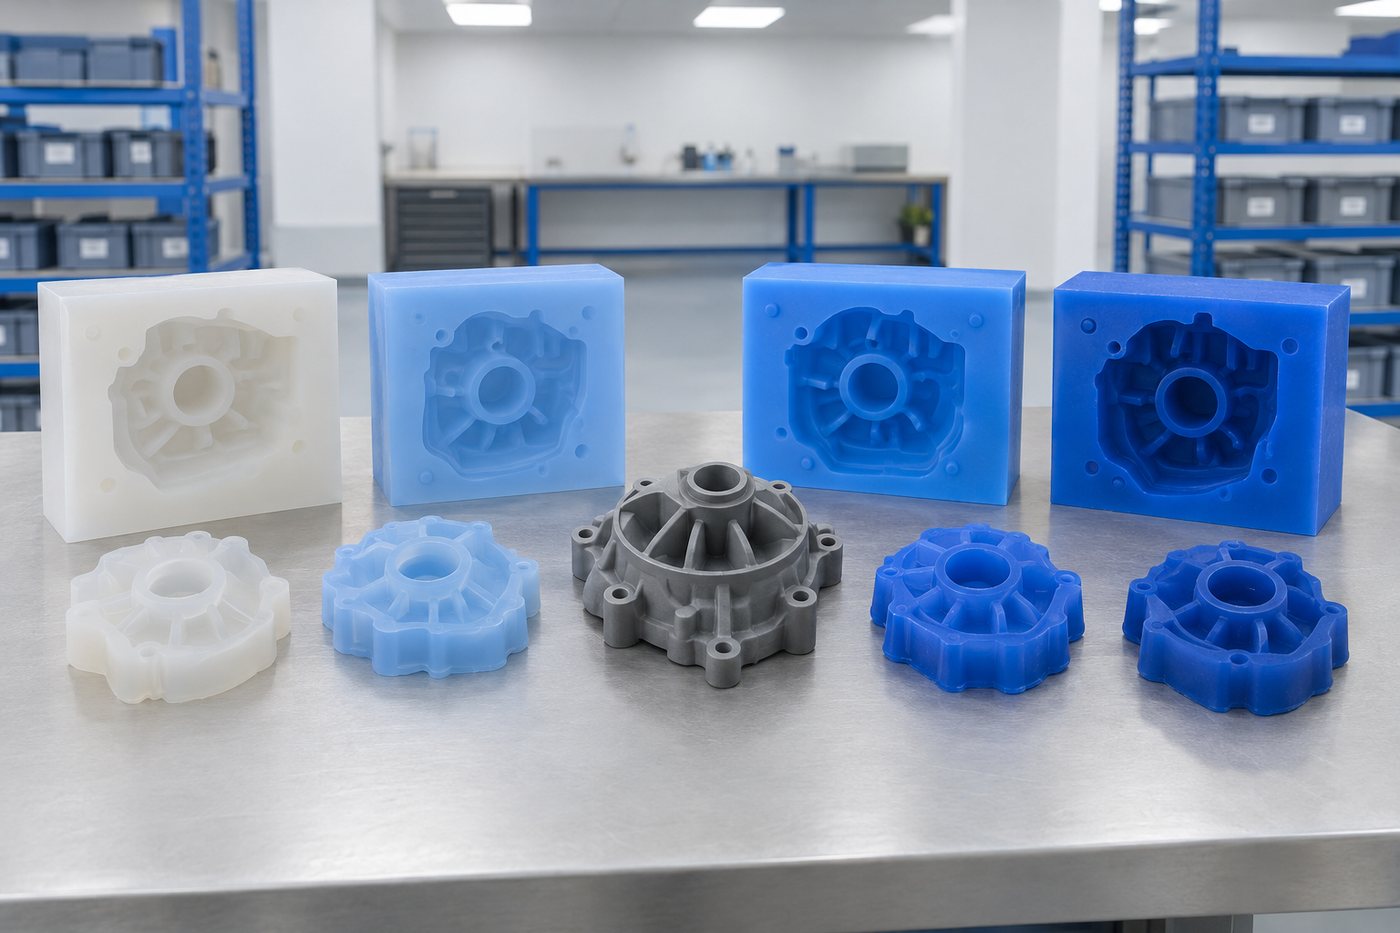
Once cured, silicone can still change over time. Heat cycles can slowly stiffen it, chemical attack can soften it, and the mixing ratio, cure conditions and age can all slightly affect the finished hardness.

We measure it rather than assume it. Hardness is read on the cured material, and the grade and reading are recorded against your order. This helps your replacement mould behave like the one it replaces, rather than simply being made from the same product name.

It also gives us a useful comparison point if a mould comes back having gone hard, become tacky or torn early. If it has stiffened over a season, that tells us something about the conditions it was working in. That insight usually helps shape the specification for its replacement.

That same record makes replacement moulds a straightforward conversation rather than a fresh development.

Replacement and spare moulds

Illustrative example: Cured silicone sample being checked with a hardness gauge

How we get there

We will determine the hardness.

Tell us about your part, what goes into the mould, how often it is pulled and who pulls it. We will recommend a grade and hardness, explain the trade-offs, and adjust our recommendation if you share any details about the duty that we did not know.

If your job sits on a boundary, a trial mould is often the sensible next step before you finalise the production specification. That's where prototype tooling helps. Finding out on a disposable mould costs less than discovering an issue with a matched set.

For hot-duty and food-contact work, the silicone grade determines the available hardness, rather than the other way round. See high-temperature moulds and food-contact moulds.

Describe the duty

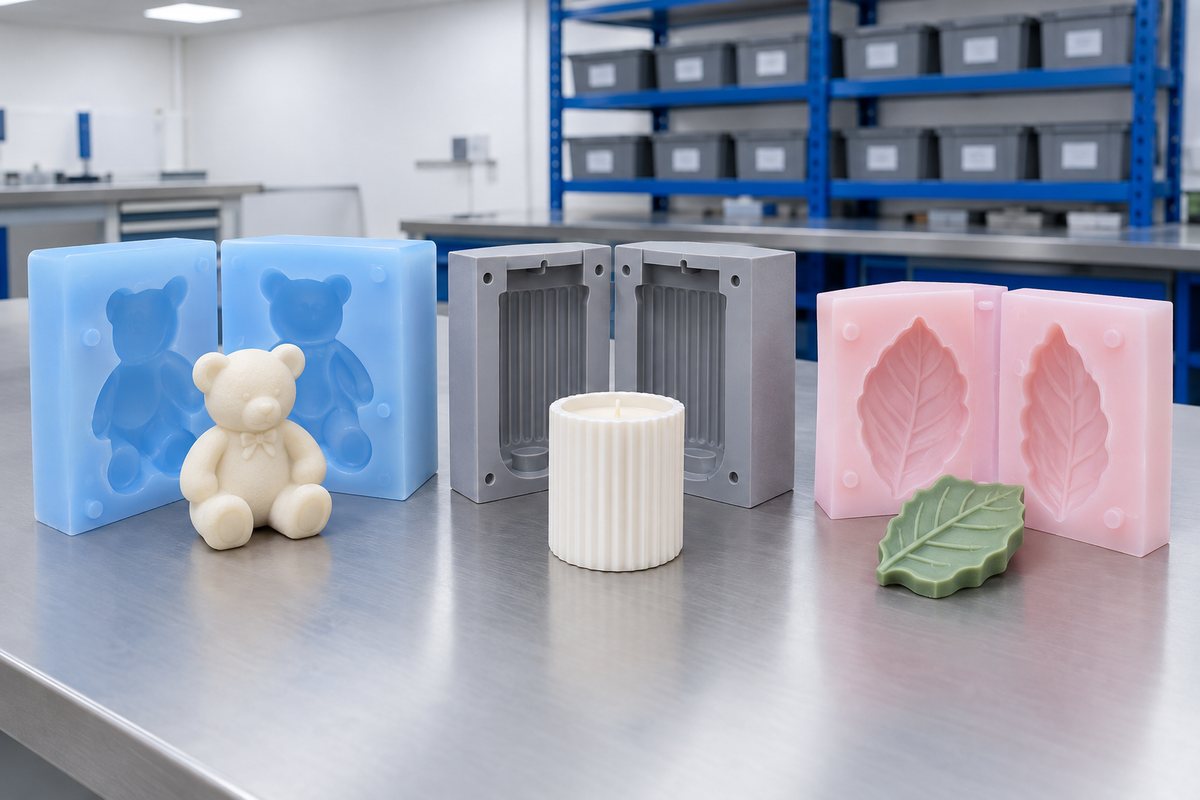
Illustrative example: Trial mould and production setup with sample castings on a bench
Using a trial mould before final production tooling

At a glance

The ideas in pictures.

Silicone hardness in everyday terms

00-30Gel insoleA10Jelly sweetA20Elastic bandA30Pencil rubberA40Shoe heelA60Tyre treadSofter: peels from undercutsFirmer: holds its shape

Swipe to see the whole diagram

A rough guide. We choose the grade for your shape, material and number of pours.

From idea to finished mould

  1. 01Photo or sampleShow us what you want to cast
  2. 02Drawing agreedWe agree the shape and split
  3. 03Master madeMachined, printed or sculpted
  4. 04Proof pourA first mould to test
  5. 05Full mouldMade once you are happy
  6. 06Kept on fileFor easy reorders

Swipe to see the whole diagram

Every mould follows the same simple route, so you always know what happens next.

Ready to start?

Tell us what you need to make, and we'll show you how to mould it.

Send us a drawing, photograph or sample. We'll come back to you with a mould strategy, a material recommendation and a price.

Real people, a real workshop

You deal with the people who make it.

No call centre and no middlemen. When you contact TCI Mouldings, you speak to the team who design, build and check your mould.

  • A real Warwickshire workshopUnit 15, Waterloo Park, Bidford-on-Avon, Alcester B50 4JG.
  • Real people on the phoneCall the team on 01789 224228, Monday to Friday.
  • The same team on every jobDesign, production and aftercare come from the people you see here.
  • Part of TCI GroupFive specialist brands, one engineering team. Visit TCI Group.
The TCI design and project office.
A stack of TCI silicone moulds.
The TCI workshop, with moulds on the bench mid-build.
  • Thomas LaneManaging Director
  • George PrestonDesign & Project Manager
  • Kelly BallingerHead of Partnerships
  • Jim AndertonProduction Manager
  • TheodoreEmployee Welfare
Meet the team